A plant in Pune’s industrial belt once showed me a monthly dashboard with every department in green. Yet customers were chasing deliveries, the stores were full and the shop floor was cluttered with part-finished work. Each department was efficient on its own. Nobody was looking at how the product actually flowed from order to dispatch.
Value stream mapping (VSM) fixes that blind spot. It is a one-page picture of material and information flow, drawn by walking the process. This post gives you a simple method you can run in a week, with a worked example and the mistakes we see most often.
What value stream mapping actually shows
A value stream map records every step a product family passes through, from customer order to delivery, along with the time each step takes and the time the product spends waiting. It also shows how information travels: how orders reach the shop floor, how schedules are set and how suppliers are called off.
The insight is nearly always the same. Value-adding work is a tiny share of total lead time. In many discrete manufacturing plants, a typical range is 1 to 5 per cent. The rest is waiting, queuing, rework and transport, which Lean calls muda (Japanese for waste). Machine-level improvement projects rarely touch this, because the delay sits between the machines.
Step 1: Choose one product family and one boundary
Do not map the whole factory. Group products that share at least 70 per cent of their process steps, then pick the family that matters most by revenue, customer complaints or delivery delays. A Chennai auto-component supplier, for instance, might choose one family of machined housings rather than all 200 part numbers.
Fix the boundary as well. “Dock to dock” (raw material receipt to finished goods dispatch) is the usual starting point. Extend to supplier and customer later.
Step 2: Walk the process backwards, at the gemba
Gemba means the actual place where work happens. Start at dispatch and walk upstream. Going backwards keeps you close to what the customer pulls, and it exposes how each step really learns what to make.
Take a stopwatch, a clipboard and one or two operators with you. Do not rely on the ERP or the standard routing sheet. Routings show planned cycle times; the floor shows what is real.
What to record at each process step
- Cycle time (CT): time to process one piece
- Changeover time (C/O): from last good piece to first good piece of the next product
- Uptime or availability, as a percentage
- Number of operators
- Batch size and yield or first-pass rate
- Inventory sitting before the step, counted in pieces and converted to days
Count the inventory yourself. Stores records and physical stock rarely agree, and that gap is itself a finding.
Step 3: Draw the current-state map
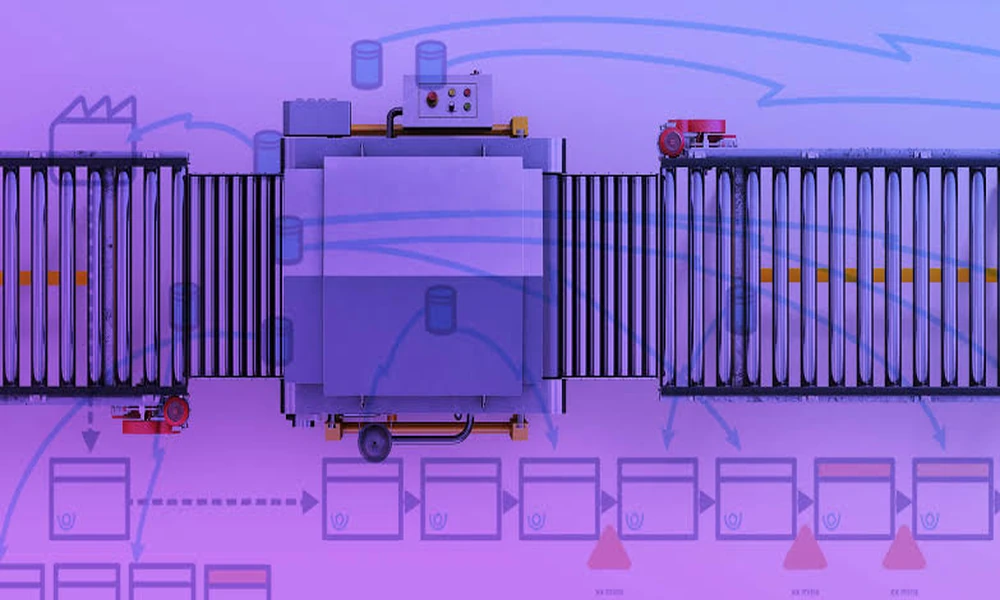
Use pencil and paper first. Software can come later. Draw customer on the right, supplier on the left, process boxes in the middle and inventory triangles between them. Below the boxes, draw a timeline: waiting time on the upper steps, processing time on the lower ones.
Then add the information flow along the top: monthly forecast, weekly schedule, daily dispatch instructions. Mark where a planner pushes a schedule into the floor rather than the next process pulling it.
A simple worked example (illustrative figures)
Suppose a plastics moulding unit has these figures for one product:
| Stage | Inventory before step | Days of stock | Process time |
| Raw material store | 12 tonnes | 6.0 | – |
| Moulding | 18,000 pieces | 4.5 | 28 sec |
| Trimming | 15,000 pieces | 3.8 | 20 sec |
| Assembly | 9,000 pieces | 2.3 | 45 sec |
| Finished goods | 12,000 pieces | 3.0 | – |
Waiting time adds up to about 19.6 days. Processing time is 93 seconds. Value-adding time is a fraction of one per cent of lead time. Nobody needs a consultant to see that moulding more efficiently will not shorten delivery. The batch sizes and push scheduling will.
Step 4: Read the map for the real losses
Look for these signals:
1. Large inventory triangles between steps, which usually point to big batches, long changeovers or unbalanced cycle times.
2. Push arrows, where a step produces to a schedule instead of to what the next step consumed.
3. Rework loops and inspection stations that hide poor process capability.
4. A pacemaker problem, where schedules go to every process instead of one point in the flow.
5. Long changeovers on the bottleneck, where SMED (single-minute exchange of dies, a method for cutting changeover time) often pays back fastest.
Mark each issue with a Kaizen burst, a small starburst sticker, so the team can see improvement ideas on the map.
Step 5: Design the future state
Ask a few direct questions. What does the customer’s takt time (available time divided by customer demand) say about the pace of the line? Where can we create continuous flow? Where must we use a supermarket (a controlled stock with Kanban replenishment)? Which single process will be the pacemaker?
Keep the future state realistic: aim for a 12-month horizon, with a target such as halving lead time, not eliminating inventory. Then convert it into a plan with owners, dates and review rhythms. This is where Hoshin Kanri, the policy deployment method that links plant priorities to team actions, helps keep the plan alive.
Common mistakes in Indian plants
- Mapping from the office. Maps drawn from ERP data miss the unrecorded buffers, rework bins and informal queues.
- Mapping everything. A plant-wide map takes weeks and nobody acts on it.
- Ignoring workforce realities. High attrition and mixed skills mean the future state needs standard work and quick training, not just a new layout.
- Forgetting the supplier end. Lumpy supplier deliveries and long transit times often drive raw material stock more than internal practice.
- Producing a poster, not a plan. If no one owns the first three actions, the map ends up on a wall.
Conclusion: start small, then build the habit
Value stream mapping works because it is simple: one product family, one walk, one page. Pick a family, map dock to dock with a cross-functional team, calculate the ratio of waiting to processing, and choose three improvements that cut lead time. Revisit the map every quarter.
If you would like a second pair of eyes, Ribcon’s lean consultants can facilitate a two- or three-day mapping workshop on your floor and help you turn the future state into a deployable plan. A conversation about one product family is a sensible place to start.